Monoblock Burners for Heaters
Oil and Gas Industry
Monoblock Burners for Heaters in Oil and Gas Industry
E&M Combustion offers monoblock burners for heaters. Heaters in the Oil & Gas industry are equipment used to heat fluids such as crude oil, natural gas, produced water, or refined products.
Their main function is to optimize processes such as phase separation, reduce crude oil viscosity, prevent hydrate formation, and improve transportation and refining efficiency.
E&M Combustion, as a thermal engineering company, designs and manufactures custom-made industrial burners for the oil and gas industry. Its main objective is to provide a technical response and the specific solutions required by its customers, while also being prepared to operate in critical areas.
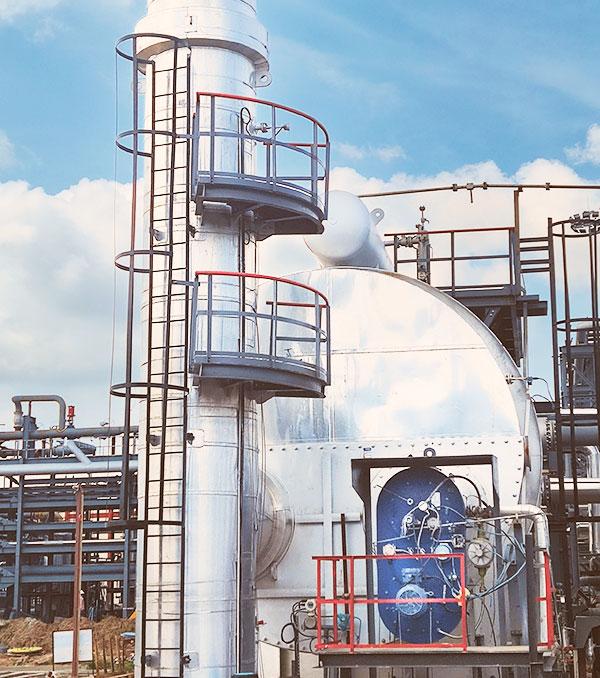
Types of Heaters in Oil & Gas
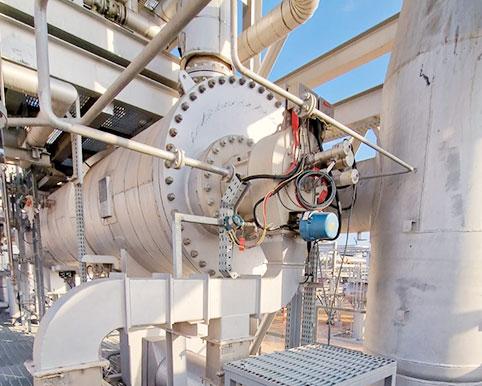
Indirect Fired Heaters
- Use a thermal fluid (such as glycol or thermal oil) to transfer heat without direct contact with the combustion source.
- Avoid contact between the fluid and the flame, reducing the risk of contamination or product degradation.
- Applications: heating natural gas before pressure regulation stations, preventing hydrates in gas pipelines.
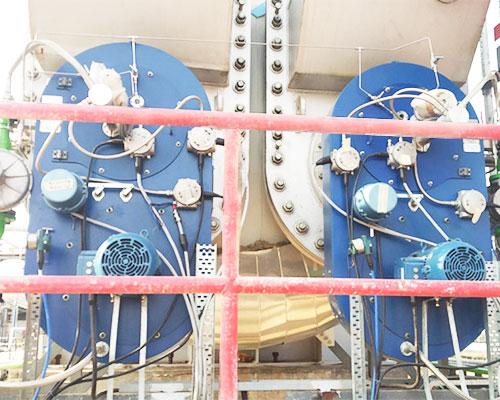
Direct Fired Heaters
- Burners directly heat the fluid through coils or combustion chambers.
- They are more efficient in heat transfer but require greater emissions control.
- Applications: heating crude oil in pipelines, refining processes, produced water treatment.
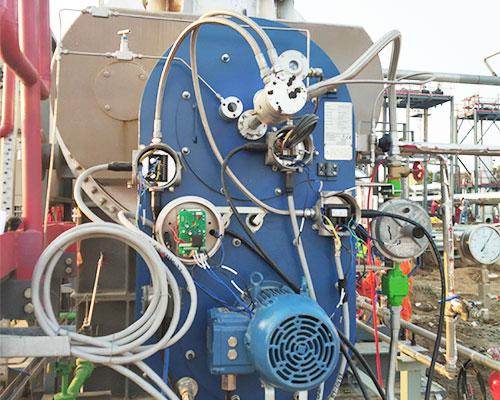
Bath Heaters (Water Bath Heaters)
- They consist of a burner that heats a bath of water or glycol, indirectly transmitting heat to a coil that transports the process fluid.
- They are used in gas pipelines to prevent ice formation and in upstream installations to heat crude oil or gas before separators.
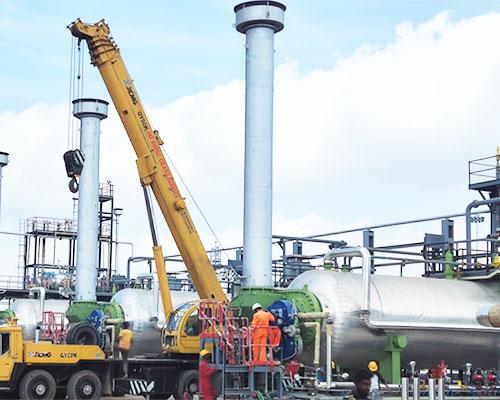
Electrically Heated Heaters
- They use electrical resistances instead of combustion.
- They are used in emissions-sensitive environments or where gas/fuel is not viable.
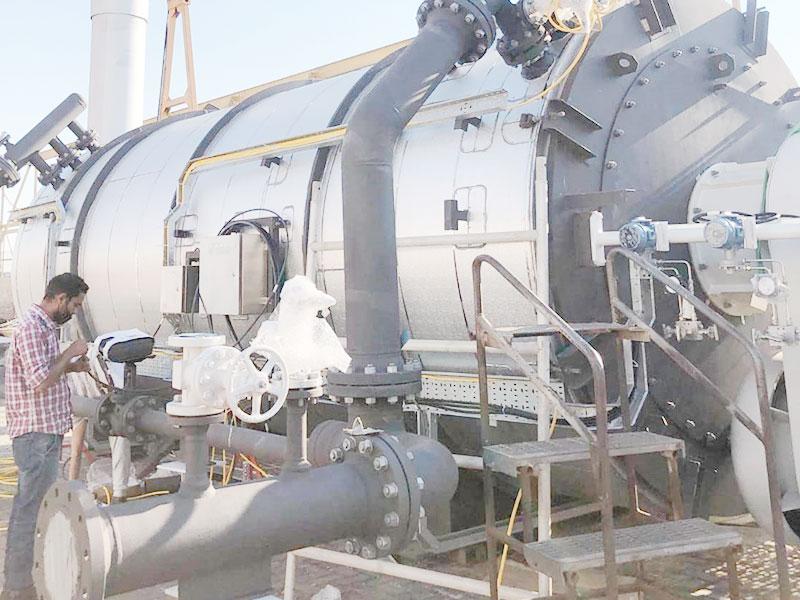
[+] Key Applications of Oil and Gas Heaters
[ 1 ] Upstream: preventing hydrate formation in gas pipelines, heating crude oil before separation.
[ 2 ] Midstream: viscosity reduction in oil pipelines, temperature maintenance in storage.
[ 3 ] Downstream: heating in refining processes, stabilizing refined products.
Features of Monoblock Burners for Heaters
E&M Combustion’s monoblock burners for heaters are designed to offer maximum performance in industrial heaters. Their compact construction and advanced technology guarantee efficiency, reliability, and ease of installation.

Compact design.
They integrate the motor and fan into a single unit, optimizing space and facilitating installation.
Wide power range. Capable of reaching up to 25 MW of thermal power, adapting to different industrial needs.
Suitable for ATEX zones. Designed to operate in environments with a risk of explosion, complying with safety regulations.
Advanced automation. Compatible with customer PLC control systems, ensuring precise and efficient regulation.
Built-in silencer.
Reduces noise levels for quieter and more comfortable operation and compliance with regulations.
Multi-fuel compatibility. They operate on a wide variety of liquid and gaseous fuels, offering great versatility.
Easy maintenance.
Accessible design to minimize downtime and optimize operation.
Low emissions and high efficiency. Advanced technology that reduces the environmental footprint and maximizes energy efficiency.
On-demand continuous pilot system. Optional according to customer needs, ensuring reliable ignition and flame maintenance in any type of operation.
Advantages of E&M Combustion Burners in Oil and Gas Applications
- Robustness and durability: constructed with high-strength materials and reinforced sheet metal thicknesses, ensuring a long service life even in extreme conditions.
- Adaptability to different types of fuel gas: designed to operate with refinery waste gases, including those with high corrosion rates.
- Custom manufacturing: customized to specific customer requirements, ensuring maximum flexibility and adaptability.
- Painted to strict standards:comply with the most rigorous customer procedures in terms of corrosion resistance and durability.
- Customized ATEX certification:adapted to the different safety levels required at each facility.
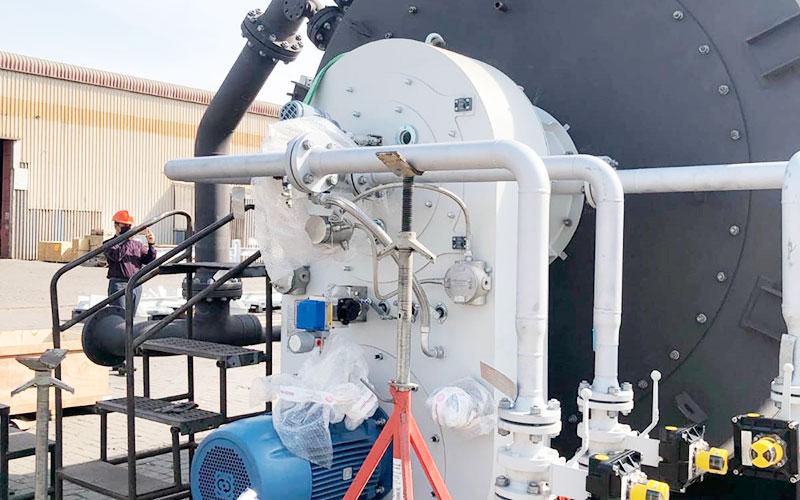
E&M Combustion guarantees, with its experience and technology in the combustion sector, the success of incorporating its burners into production processes.
Equipment for Atex Zones
Our burners are designed to operate safely in explosive atmospheres (zones classified as ATEX), complying with European ATEX 2014/34/EU regulations and international safety standards.
This equipment features certified electrical and mechanical components to prevent accidental ignition, ensuring reliable operation in environments where the presence of flammable gases, vapors, or combustible dust poses a risk.
In addition, we adapt our burners to different ATEX protection levels (Zone 1, Zone 2, EExd, EExde), ensuring compatibility with the specific requirements of each industrial facility.
E&M Combustion’s ATEX burners are constructed with certified materials and designed to operate safely in these conditions, guaranteeing:
- Protection against ignition in explosive atmospheres.
- Compliance with international safety regulations.
- Electrical and mechanical components specially designed for ATEX zones.
- Compliance with international safety regulations.
Duoblock Burner Options
In addition to monoblock burners, E&M Combustion offers duoblock burners, ideal for applications requiring the use of preheated air to improve energy efficiency and optimize combustion.
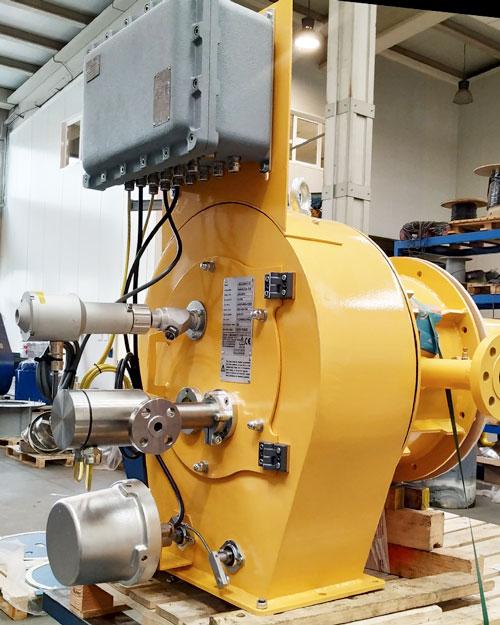
Advantages of duoblock burners:
✔ Compatibility with preheated air, increasing thermal efficiency and reducing fuel consumption.
✔ High adaptability, with customized configurations based on the specific operating conditions of each industry.
✔ Ideal option for systems with two fans in parallel, allowing one to operate with one on and the other on standby, ensuring redundancy and continuity in the process.
Documents (PDF)
For more information, please download the product brochure:
“MONOBLOCK BURNERS FOR HEATERS – Oil and Gas Industry”
E&M Combustión manufactures custom burners for heaters. Call us for more information.